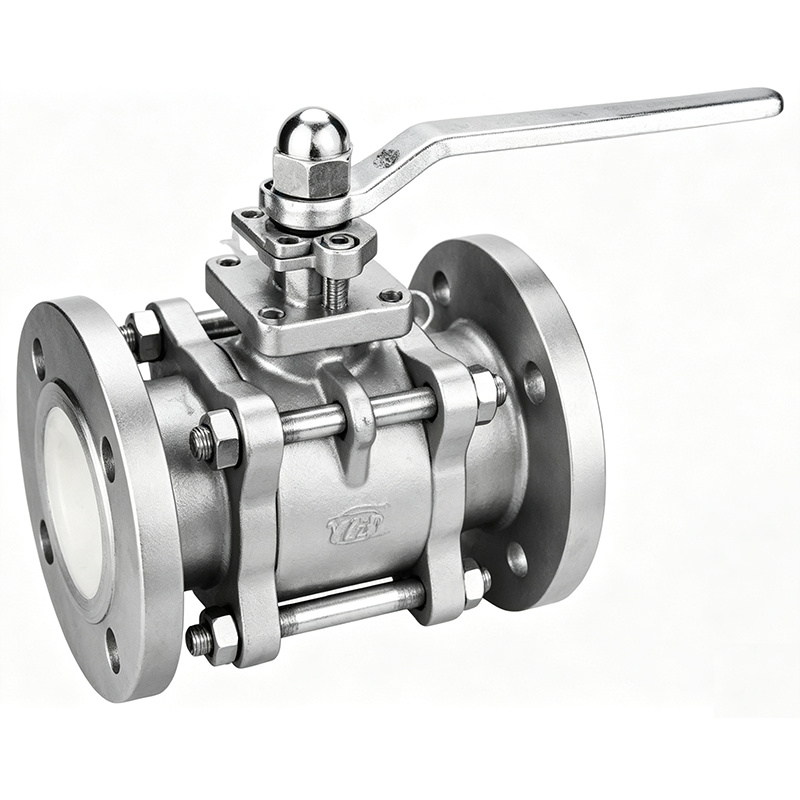
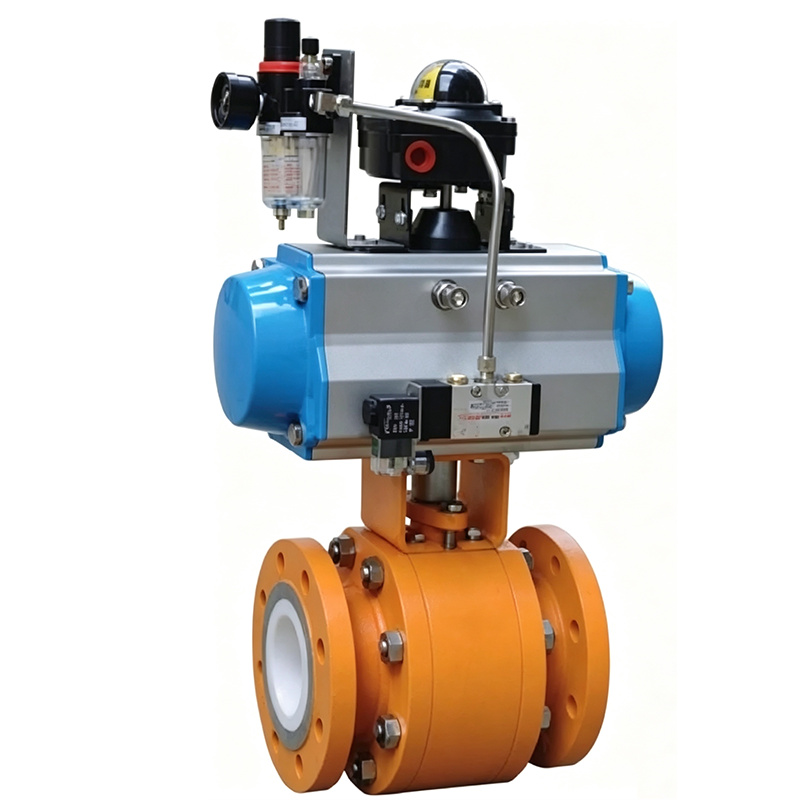
Product Description
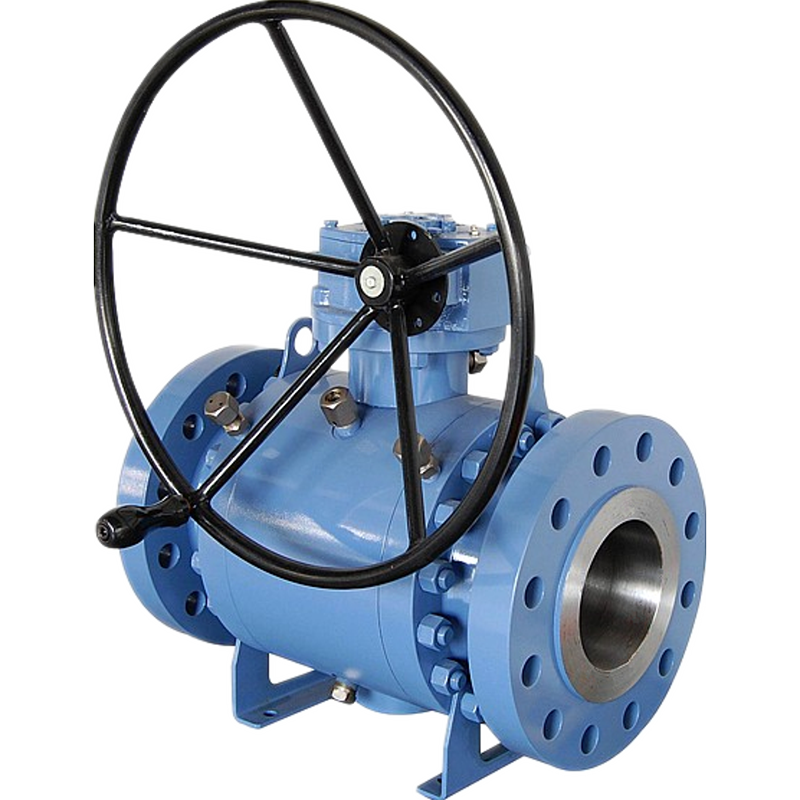
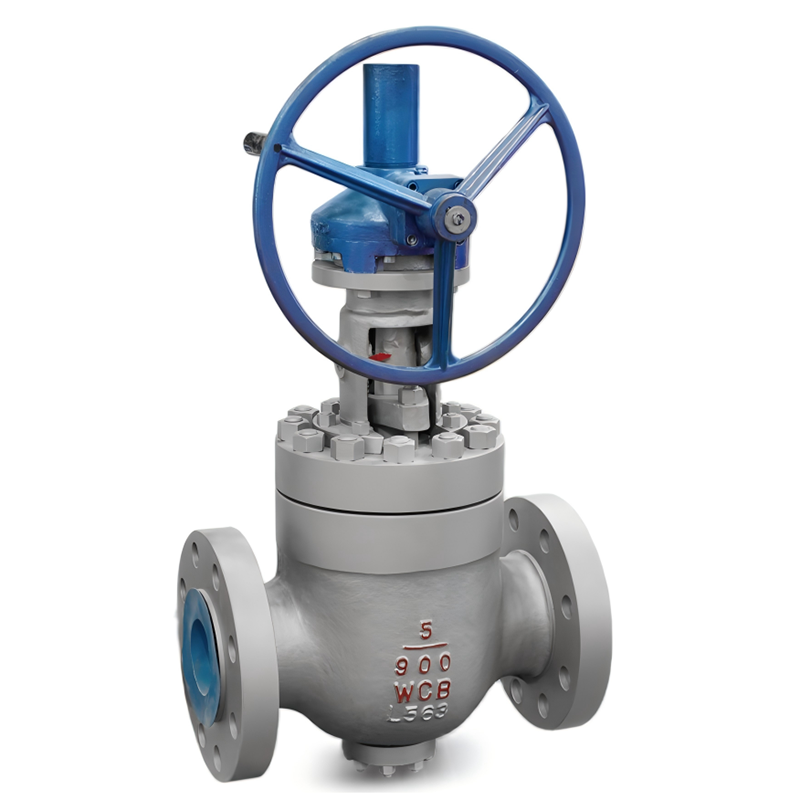
1. Ceramic ball valves feature ball cores manufactured from high-performance structural ceramics. Boasting excellent wear resistance with hardness above HRC88 and corrosion resistance, they are suitable for harsh working conditions with heavy erosion, strong corrosion and particle laden media.
2. The ball core is made of alumina with AL2O3 content of 95%, 99% or 99.5% or zirconia including 3Y-TZP and Ce-TZP. Sintered at high temperature, it delivers extremely high surface hardness and chemical stability.
3. The valve seat adopts a special elastic structure or metal sealing structure to achieve reliable sealing when matched with the ceramic ball core. The valve body material can be selected according to medium characteristics.
4. The valve body design meets the requirements of ASME B16.34 standard
5. Ceramic ball valves offer long service life and low maintenance cost. They are especially suitable for slurry services in industries such as desulfurization and denitrification, coal chemical industry, mining and metallurgy, and paper making.
Features & Benefits
1. Ceramic ball core: Made of high quality structural ceramic material. Its hardness is close to diamond, and its wear resistance is more than 10 times that of stainless steel for longer service life.
2. Excellent corrosion resistance: Ceramic features strong chemical inertness and can resist corrosion from most acids, alkalis and salts.
3. Anti clogging design: The smooth ceramic surface does not adhere to media and resists scaling and jamming, suitable for complex media prone to crystallization and containing fiber particles.
4. Reliable sealing: The valve seat adopts elastic or special sealing design, which fits tightly with the ceramic ball core for low leakage rate.
5. Wide applicable temperature range: Ceramic and sealing materials can be selected as required, with operating temperature ranging from -40℃ to +400℃.